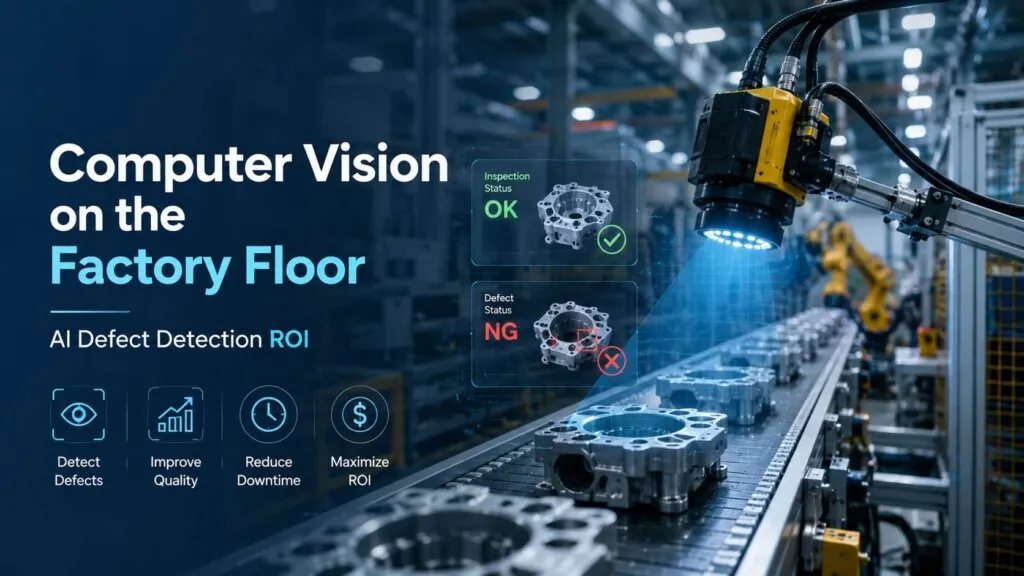
AI defect detection has moved from experiment to everyday production tool in electronics, automotive, pharmaceutical, food and beverage, and packaging plants. Vendors publish impressive accuracy and payback figures. What those figures rarely explain is why some deployments reach them while others stall as pilots. This guide covers what actually decides the outcome of a computer vision in manufacturing project: the ROI streams, the data foundation, the inference hardware, the integrations and the long-term model care.
Our team has worked on AI defect detection systems for manufacturing clients, and one pattern keeps repeating. The model itself is rarely the limiting factor. The limiting factor is usually the data infrastructure needed to train, deploy and maintain it. Close behind is the integration work that connects a working inspector to quality systems, production reporting and the people who run the plant.
Key Takeaways
- AI defect detection learns from labeled images, so it handles defect variation that rule-based machine vision quality control struggles with.
- ROI comes from four streams: labor, scrap and rework, warranty and recall avoidance, and process data.
- Training data coverage and labeling quality matter more than model architecture.
- Line-speed inspection needs edge inference with millisecond latency budgets, not a cloud round-trip.
- Integration with MES, QMS and ERP systems turns inspection results into usable quality records.
- Drift monitoring and retraining keep accuracy stable as products, materials and lighting change.
What Is AI Defect Detection?
AI defect detection is the use of trained machine learning models to find flaws in products from camera images. The model looks at each part and classifies it as good or defective. Many systems also locate the defect and label its type. It is a branch of computer vision applied to quality control.
The difference from earlier approaches is how the inspection logic is created. A rule-based system is programmed by an engineer. An AI system learns from examples. That single change explains most of its strengths and most of its risks.
How Earlier Machine Vision Worked
Traditional machine vision relied on rules. An engineer defined every inspection criterion in terms of pixel thresholds, shape boundaries and colour ranges. These systems work well for fixed, clearly defined defects against consistent backgrounds. Electronics lines have used automated optical inspection this way for decades.
Rule-based systems break down when defect appearance varies. They also struggle when product geometry changes between SKUs, or when lighting shifts across shifts. Reprogramming them for a new product line takes engineering effort and offline time.
Why Learned Models Generalize Better
AI defect detection replaces explicit rules with models trained on labeled images of good and defective parts. The model can generalize to defect variations that the training set did not explicitly include. A rigid rule, by contrast, fails on anything outside its programmed boundary.
This is why visual inspection automation based on deep learning is replacing older machine vision quality control in high-mix, variable-surface and organic-product contexts. Those are exactly the settings where rules underperformed.
| Aspect | Rule-based vision | AI defect detection |
|---|---|---|
| Logic source | Hand-coded rules | Labeled examples |
| Defect variation | Brittle | Generalizes |
| New SKU effort | Reprogramming | Retraining |
| Data needed | Little | Curated image sets |
| Ongoing care | Rule updates | Drift monitoring |
The Four ROI Streams of AI Defect Detection
Computer vision in manufacturing ROI does not come from a single source. Understanding the four value streams helps set realistic payback expectations before a project begins. It avoids discovering a gap between projected and actual returns halfway through.
The payback timeline depends on which stream dominates in a given plant. An electronics maker with thin margins and high returns will see a different timeline than a food producer focused on recall risk. Both may still deploy technically similar AI defect detection infrastructure. That is why our team recommends building a simple ROI model per line before committing to scope.
Labor Cost Reduction
With AI defect detection in place, reassigning manual inspection staff is often the fastest-realizing ROI component. Inspectors can move to exception handling and process improvement roles instead of repetitive visual scanning. This stream is also the easiest to model, since current inspection headcount and labor rates are already known.
Scrap and Rework Reduction With AI Defect Detection
Manual visual inspection is limited by fatigue and by the natural limits of human consistency at line speed. Automated quality inspection runs at a consistent level around the clock. It can catch defects that tired eyes miss, so less defective product reaches final assembly or the customer. In material-intensive plants, scrap and rework savings can rival labor savings.
Warranty and Recall Avoidance
The largest ROI component is also the hardest to model in advance. It is the reduction in warranty claims and recalls that comes from catching defects before they ship. Automotive and medical device makers know how expensive a single recall can be. The same logic applies at smaller scale to any product with real field failure risk.
Process and Traceability Data
Every AI defect detection inspection produces structured data: defect type, location, frequency and timing. Manual logs rarely capture this in usable form. Linked to upstream process parameters, it supports root-cause analysis, predictive quality modelling and audit documentation. This value often outlasts the inspection function itself.
Why Data Infrastructure Decides AI Defect Detection ROI
The gap between a working model and one that delivers business value usually comes down to early data decisions. A model trained on an unrepresentative dataset will look good in evaluation. It will then fail on the full range of defects it meets on a live line. Over-represented common defects and missing rare ones are the classic cause.
Training Data Quality and Coverage
For AI defect detection, a representative training set needs both good images and good labels. That means working with experienced quality engineers who know what a defect looks like and why it matters. Simply collecting historical images and treating them as ground truth is not enough.
Our Data and AI services team treats training data preparation as an engineering task in its own right. A well-designed model trained on poor data will underperform a simpler model trained on data that reflects real production conditions. Useful practices include:
- A shared defect taxonomy agreed with quality engineers before labeling starts.
- Deliberate collection of rare but costly defect types.
- Images from every shift, SKU and lighting condition.
- Double labeling on a sample to measure label agreement.
- A held-out test set that is never used for training.
Real-Time AI Defect Detection Inference
AI defect detection at line speed needs inference that processes frames before a part leaves the inspection station. This is not a generic cloud AI workload. It needs edge computing close to the line, with latency budgets in milliseconds rather than the seconds a cloud round-trip can take.
Our DevOps and cloud engineering practice designs the edge-to-cloud architecture at the start of each visual inspection automation engagement. Getting inference latency wrong is a common reason sound deployments fail to run at full production speed. The cloud still has a role: model training, fleet updates and long-term analytics live there.
Machine Vision Quality Control and System Integration
A machine vision quality control system that flags defects but does not connect to the MES, QMS or ERP creates more work than it removes. Quality engineers end up reconciling data from a disconnected system with the records their other tools expect. Our application development teams treat these integrations as a core deliverable, not an add-on for later.
Integration depth matters most for the traceability and process data streams. An AI defect detection system that logs results into its own closed database delivers less value. One that routes data into the quality workflows engineers already use delivers far more. Typical integration points include:
- Reject signals to PLCs or diverters on the line.
- Defect records written to the QMS with images attached.
- Lot and serial traceability linked in the MES.
- Shift and line dashboards for supervisors.
- Exports to analytics platforms for process engineers.
Where plants already run SCADA and IoT sensor networks, inspection data can be joined with machine signals. This opens the door to predictive maintenance and even a digital twin of the line, which our digital twin solutions team builds on top of the same data foundation.
Keeping AI Defect Detection Models Accurate Over Time
A computer vision in manufacturing deployment that performs well at launch can degrade as conditions change. New product variants, different raw material suppliers, equipment ageing and slow camera drift all affect what the model sees. Many of these shifts are gradual. They can go unnoticed until detection rates have already fallen.
This drift problem is why our MLOps practice treats monitoring and retraining as a core part of every engagement. It is not an optional add-on to consider after go-live. Our related article on AI project failure after launch explains why so many models degrade quietly in production.
What to Monitor in AI Defect Detection
Regular monitoring gives quality teams early warning before drift shows up as field escapes or rework. The core signals are:
- Detection confidence distributions per defect class.
- False positive and false negative rates from operator review.
- Comparison against baseline validation metrics.
- Input image statistics such as brightness and focus.
- Volume of parts routed to manual review.
A structured approach to model risk, such as the NIST AI Risk Management Framework, helps teams document these controls. This discipline separates deployments that sustain their value over years from those that slowly decay.
Implementation Sequencing That Reduces Deployment Risk
The order in which AI defect detection capabilities are deployed matters more than most plans assume. A good first target combines high business impact with clean, consistent defect appearance. High impact means either high frequency or high cost per escape. That first use case earns operational trust and generates feedback data for harder defect types.
Trying to deploy facility-wide automated quality inspection from day one usually creates a complex, slow project. It takes longer to show results and generates more friction than a phased approach. Our team typically recommends this sequence:
- Audit inspection processes and rank defect categories by impact.
- Run lighting and camera trials at the real station.
- Build the dataset and train a first model for one or two defects.
- Validate the full data-to-dashboard pipeline on one line.
- Integrate with MES and QMS, then expand to more lines and defects.
Lighting and Camera Specification
The quality of an AI defect detection model is bounded by the quality of its images. Getting lighting and cameras right is a prerequisite for everything downstream. Inconsistent lighting is one of the most common root causes of underperforming visual inspection automation. Even a well-trained model cannot detect a defect it cannot see.
For every AI defect detection station, we run structured lighting trials at the actual inspection station before finalizing hardware. Ambient factory light, vibration, heat and product reflectivity all affect what works in practice. Backlights, dome lights, line-scan cameras and polarizing filters each suit different surfaces.
Cross-Industry Patterns in AI Defect Detection
Across industries, computer vision in manufacturing quality applications share a common technical structure. They vary in which defects matter most and in the regulatory context around inspection data. The table below summarizes the patterns our team sees most often.
| Industry | Typical focus | Key constraint |
|---|---|---|
| Electronics | Solder, component presence | Very high throughput |
| Pharmaceutical | Packaging, fill, labels | Validation and audit trails |
| Automotive | Paint, machined surfaces | Mixed camera setups |
| Food and beverage | Foreign matter, shape | Natural variation |
| Packaging | Seals, print quality | Fast changeovers |
Regulated and Variable Products
Pharmaceutical manufacturers face stricter requirements around traceability and validation documentation. Their AI defect detection deployments may need to satisfy regulator audit expectations as well as operational targets. That shapes how datasets, model versions and results are stored.
Food and beverage producers face a different AI defect detection challenge. "Defective" and "acceptable" are often a continuum, especially for organic products. The model must learn acceptable variation ranges rather than deviations from a fixed ideal. Automotive plants often need separate stations for cosmetic paint inspection and dimensional checks, since each needs different optics. Our manufacturing industry solutions page covers how these projects fit broader plant modernization.
Where ICANIO Fits in Manufacturing Vision Projects
ICANIO engagements usually begin with an inspection process audit. The goal is to identify which defect categories and line segments are the highest-value targets before any hardware is specified. Only then does model training begin.
Our teams in India, the USA and Singapore combine data engineering, application development, DevOps and MLOps for these projects. That mix matters because AI defect detection touches cameras, edge devices, cloud pipelines and plant software at once. For a broader view of plant modernization, see our article on manufacturing digital transformation.
Conclusion
AI defect detection delivers real value when the whole system is engineered, not just the model. Representative training data, edge inference sized for line speed, deep integration with quality systems and steady drift monitoring decide whether a pilot becomes a production asset.
Start small, prove one line end to end, and expand with the trust and data that first win creates. That phased path is the most reliable way to turn machine vision quality control into lasting ROI.
If you are planning an inspection project, contact ICANIO to talk through your defects, lines and data with our team.
References
- Computer vision overview, Wikipedia
- Machine vision, Wikipedia
- Automated optical inspection, Wikipedia
- Edge computing, Wikipedia
- NIST AI Risk Management Framework
Frequently asked questions
How accurate is AI defect detection compared to manual inspection?
Accuracy depends on the defect class, image quality and training data. For well-defined defects with good lighting and representative data, AI defect detection can be very accurate and, unlike people, does not tire across a long shift. The right way to judge it is a side-by-side trial on your own parts, measuring false positives and false negatives against expert review before you commit to full deployment.
How long does automated quality inspection take to pay back?
Payback varies with line complexity, defect costs, labor rates and integration depth. Plants where labor and scrap savings dominate tend to see returns sooner, while recall avoidance is harder to forecast. Our team recommends building a simple per-line ROI model covering all four value streams before scoping, so expectations are realistic and the first phase targets the line with the clearest return.
How does AI defect detection differ from traditional machine vision?
Traditional machine vision uses hand-coded rules such as pixel thresholds and shape limits, which fail on variations outside those boundaries. AI defect detection learns from labeled images of good and bad parts, so it generalizes to variations it was never explicitly programmed for. The trade-off is that it needs curated training data and ongoing monitoring for drift as products and conditions change.
Why do some computer vision in manufacturing pilots fail to scale?
The most common reasons are thin training data coverage, inference hardware that cannot meet line-speed latency, and missing integration with MES, QMS or ERP systems. These are infrastructure and process decisions rather than model quality problems. Pilots also stall when nobody owns drift monitoring after launch, so accuracy slowly falls and operators lose trust in the system.
How is model accuracy maintained after deployment?
Ongoing MLOps monitoring tracks confidence distributions, false positive and negative rates, and input image statistics against a baseline. When drift appears, the team collects new labeled images from current production and retrains. Each new model version is validated on a held-out test set before release, and versions are tracked so results stay auditable for quality and regulatory reviews.
What hardware does AI defect detection need?
A typical station needs industrial cameras, controlled lighting, an edge computer with a GPU or vision accelerator, and a connection to line controls for rejects. The exact choice depends on part size, line speed and surface type. Lighting trials at the real station are the best way to finalize the specification, since ambient light and reflectivity often change what works.